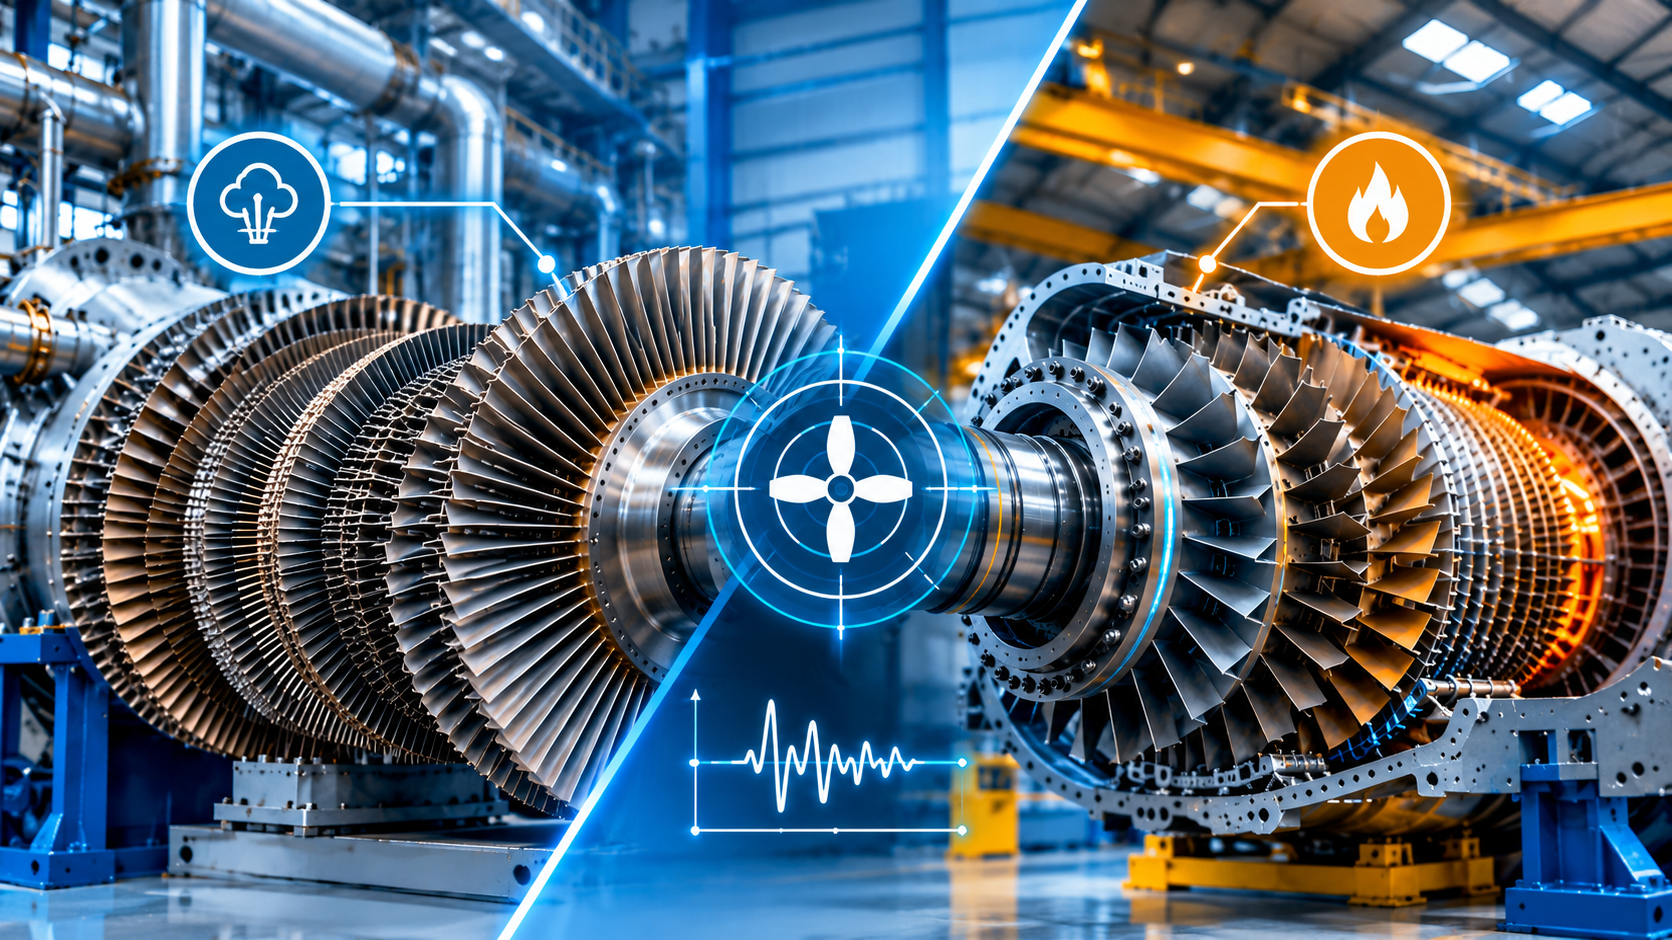
A turbine coupling can be aligned while the internal turbine geometry is still wrong. Shaft alignment receives considerable attention during turbine overhaul. Correct coupling alignment is essential — but it is only part of the story.
Inside a steam turbine, the rotor passes through a series of geometrically related components including:
- Bearings
- Diaphragms
- Gland seals
- Packing/seal bores
- Blade paths
- Casing sections
- Oil guards
- Couplings
These components must be correctly positioned relative to the intended turbine rotor centreline.
If the internal geometry is incorrect, it is possible to achieve acceptable coupling alignment while still having improper internal clearances or rotor-to-stationary-component relationships.
That can contribute to:
- Rotor rub
- Seal contact
- Uneven clearances
- Efficiency loss
- Elevated vibration
- Thermal sensitivity
- Difficult startup
- Component damage
This is why turbine casing and diaphragm alignment is a critical activity during major overhaul.
What Is the Turbine Centreline?
The turbine centreline is the geometric reference around which the stationary internal components and rotor system are aligned.
Conceptually, engineers want:
Bearing centre → Seal centre → Diaphragm centre → Gland centre → Bearing centre
to form the required designed relationship.
The objective is not necessarily to create a mathematically perfect straight line in every case.
OEM design targets may intentionally incorporate:
- Bearing elevation
- Catenary considerations
- Thermal growth
- Casing movement
- Rotor deflection
- Operating-position corrections
Therefore the correct reference is the design/OEM alignment condition, not simply “zero everywhere.”
What Is Diaphragm Alignment?
Steam turbine diaphragms separate pressure stages and carry stationary steam-path components. The rotor passes through the diaphragm bores with carefully controlled clearances.
During overhaul, diaphragms may be:
- Removed
- Cleaned
- Inspected
- Repaired
- Reinstalled
- Repacked or adjusted
Their positions must then be verified relative to the intended rotor centreline.
An incorrectly positioned diaphragm can reduce radial clearance between rotating and stationary components.
Even a comparatively small geometric error can matter in a high-speed turbine.
Components Commonly Included in Geometric Alignment
Depending on turbine design and outage scope, measurement may include:
- Bearing bores
- Diaphragm bores
- Gland/seal bores
- Packing bores
- Oil guards
- Casing bores
- Rotor seal locations
- Coupling references
- Valve/chest geometry where applicable
- Horizontal joint surfaces
- Casing flatness
Laser-based bore measurement systems are used in the industry for steam and gas turbine, compressor and engine bore alignment. A documented turbine overhaul using a laser bore-alignment system measured bearing bores, stuffing boxes, seals, packing and housing bores and evaluated both top-half-off and assembled conditions.
Why Traditional Methods Can Be Difficult
Historically, turbine internal alignment has often been performed using methods such as:
- Piano wire
- Dummy shafts
- Optical instruments
- Mechanical micrometers
- Tight wire methods
These methods can work well when correctly implemented by experienced personnel. However, they may have practical limitations.
- Wire Sag: A long wire does not remain perfectly straight under gravity. The sag must be properly calculated or compensated.
- Accessibility: Measurements inside large turbine casings may be difficult.
- Setup Time: Mechanical reference systems can require significant setup and repeated adjustment.
- Human Reading Error: Manual measurement can depend significantly on operator technique.
- Corrections During Measurement: Some traditional methods require substantial dismantling or resetting before components can be moved and rechecked.
Modern laser geometric alignment can simplify the establishment of a stable reference and provide digitally documented measurement results.
How Laser Bore Alignment Works
In simplified form:
1. Establish the Reference
A laser beam is established according to selected turbine reference points. These may be based on OEM-defined bearing positions or other geometric references.
2. Measure Each Bore
A detector or target is positioned at different axial locations. The system measures the horizontal and vertical displacement of each bore centre relative to the laser reference.
3. Build the Geometric Profile
The measurements create a representation of component positions along the turbine axis.
4. Compare Against Required Targets
Each diaphragm, seal or bearing bore can be compared with OEM or project tolerances.
5. Calculate Corrections
Required horizontal and vertical movements can be established.
6. Correct and Re-Measure
Components are adjusted and measurements repeated to verify the final condition.
Why “Tops-Off” and “Tops-On” Measurements Can Matter
Large turbine casings and diaphragms are massive structures. Removing the upper casing changes loading. When the top half is reinstalled, the weight and bolting condition can alter the geometry.
An industry case study involving a large 550 MW steam turbine demonstrated measurable differences between top-half-off and top-half-on internal positions because the upper components affected the turbine centreline. This illustrates an important principle:
The geometry measured with the turbine open may not be identical to the geometry of the assembled turbine.
For critical overhaul work, measurement strategy should therefore follow OEM requirements and consider casing assembly condition.
Bearing Bore Alignment
Bearings establish the rotor support geometry. Their positions influence:
- Rotor centreline
- Coupling alignment
- Bearing loading
- Oil-film behaviour
- Seal clearances
- Rotor dynamic response
Bearing bore position should therefore be understood before simply adjusting diaphragms around an assumed centreline.
Diaphragm Bore Alignment
Once appropriate references are established, diaphragm centres can be measured relative to the required rotor axis. Corrections may involve:
- Keys
- Shims
- Adjusting screws
- Support surfaces
- Fit corrections
- Other OEM-approved methods
The correction method depends entirely on turbine construction. The important requirement is accurate as-found and as-left documentation.
Seal and Gland Alignment
Labyrinth seals and turbine gland systems often operate with small radial clearances. Incorrect alignment can lead to:
- Rubbing
- Local heating
- Seal wear
- Increased leakage
- Efficiency deterioration
- Vibration
- Rotor bow in severe cases
Checking seal and gland bore geometry during an outage can therefore prevent problems that otherwise appear only after the turbine is closed and returned to operation.
Casing Alignment and Geometry
Turbine alignment is not restricted to circular bores. Depending on scope, geometric measurement can also investigate:
- Horizontal joint flatness
- Casing distortion
- Parallelism
- Straightness
- Bearing pedestal elevation
- Flange geometry
- Foundation movement
Laser geometric measurement techniques are used industrially for straightness, flatness, bore alignment, parallelism and related machine geometry measurements.
Thermal Growth Cannot Be Ignored
A turbine aligned perfectly at ambient temperature does not remain geometrically identical when operating.
During operation:
- Casing temperature rises
- Bearings and pedestals expand
- Piping loads change
- Rotor temperature changes
- Supports expand
- The entire machine may move relative to its cold position
Precision alignment must therefore account for the required operating condition.
ACOEM alignment technology, for example, supports target values and measurements used to compensate for thermal growth or dynamic movement rather than assuming zero cold offset is always correct.
Internal Alignment and Coupling Alignment Must Be Treated as One System
Consider a turbine-generator train. The overhaul team successfully aligns the turbine-to-generator coupling. But one group of diaphragms is vertically displaced relative to the rotor path. The coupling result may appear excellent while internal clearance remains incorrect. Conversely, internal alignment can be correct while the final shaft coupling alignment is unacceptable.
A high-quality overhaul therefore considers the complete geometry:
Internal turbine geometry
↓
Bearing centreline
↓
Rotor position
↓
Coupling alignment
↓
Driven equipment
One measurement cannot substitute for all the others.
Pre-Alignment Checks Matter
Before final shaft alignment, experienced engineers should also evaluate factors such as:
- Soft foot
- Pipe strain
- Foundation condition
- Bearing clearances
- Coupling runout
- Shaft runout
- Thermal movement
Modern alignment tools can support checks including axial/radial flange runout, bearing clearance, soft foot, pipe-induced movement, casing thermal movement and bent-shaft indications.
What Can Happen When Internal Alignment Is Wrong?
Potential symptoms include:
High Vibration
Rotor-to-stator interaction or altered bearing loads can increase vibration.
Repeated Seal Rubbing
A seal may be replaced several times while the actual geometric cause remains.
Startup Vibration
Clearance problems may become more severe as the turbine passes through thermal transient conditions.
Efficiency Loss
Incorrect steam-path clearances can increase leakage.
Uneven Bearing Loading
Incorrect bearing elevations can alter load distribution.
Rotor Bow
Severe or persistent rubbing may contribute to thermal distortion of the rotor.
Difficult Commissioning
A turbine may require repeated shutdowns after overhaul because alignment problems only become apparent during operation.
This is why accurate internal geometry measurement during the planned outage is much less expensive than troubleshooting after startup.
As-Found Measurements Are Extremely Valuable
Before moving components, record their existing condition. An as-found report can reveal:
- Which components had moved
- Whether previous alignment was incorrect
- Whether casing distortion is developing
- Whether bearing elevation changed
- Whether recurring rub locations correlate with geometric errors
Without as-found data, valuable root-cause evidence can be lost as soon as the first component is adjusted.
As-Left Documentation
The final alignment report should clearly identify:
- Reference points
- Measurement method
- Instrument details
- Calibration status where applicable
- Bore locations
- Horizontal deviations
- Vertical deviations
- OEM/project tolerances
- Corrections performed
- Final as-left results
- Any unresolved deviations
This documentation becomes invaluable at the next overhaul.
VIBSpECTRUM Turbine Geometric Alignment Capability
VIBSpECTRUM provides precision machinery and turbine alignment services for power generation and industrial turbomachinery.
Capabilities can include:
- Turbine casing alignment
- Diaphragm bore alignment
- Bearing bore alignment
- Seal and gland alignment
- Geometric centreline measurement
- Laser bore alignment
- Straightness measurement
- Flatness measurement
- Shaft coupling alignment
- Thermal-growth compensation
- Runout measurement
- Soft-foot investigation
- Multi-machine train alignment
- As-found/as-left reporting
Our objective is not simply to obtain a green indication on a laser alignment screen.
It is to ensure that the turbine’s internal geometry, rotor centreline and connected shaft train are treated as one integrated mechanical system.
Frequently Asked Questions
What is turbine diaphragm alignment?
It is the measurement and correction of turbine diaphragm bore positions relative to the required rotor centreline.
Is coupling alignment enough during a turbine overhaul?
No. Coupling alignment does not confirm that internal diaphragms, bearings, seals and casing geometry are correct.
Can turbine bores be measured with lasers?
Yes. Laser-based systems are widely used for bearing, diaphragm, seal and casing bore alignment.
Why measure with the top casing installed and removed?
Large casing structures can change geometry under the weight and constraints of the upper casing. The required measurement method depends on OEM procedure.
Should every diaphragm be set exactly to zero?
Not necessarily. OEM-specific targets may account for thermal growth, rotor behaviour and design geometry.
When should turbine internal alignment be performed?
Typically during major overhaul, after relevant inspection/repair activities and before final turbine closure, according to the overhaul procedure.